1060
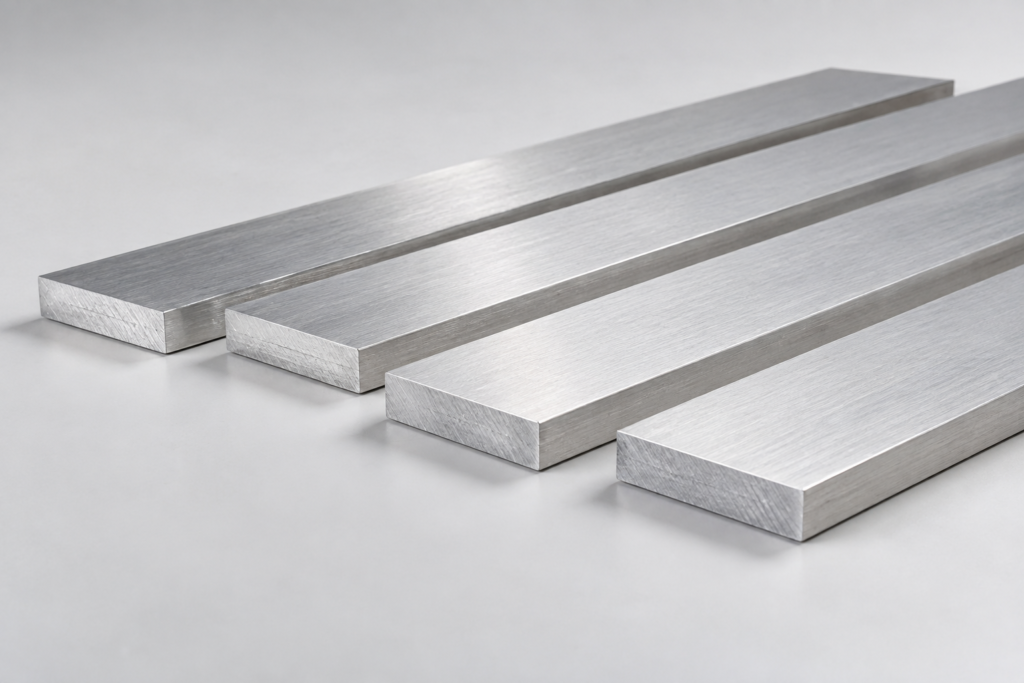
Алуминиева плочаCommercially Pure Aluminum
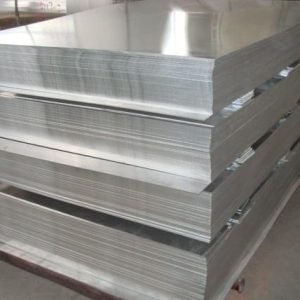
High aluminum purity combines low weight with excellent formability and thermal and electrical conductivity. Suitable for components that prioritize fabrication, surface finish and heat or current transfer over structural strength.
01 / MATERIAL OVERVIEWUnderstanding 1060 Алуминий
1060 is a 1xxx-series commercially pure aluminum grade with a minimum aluminum content of 99.60%. Its strengths include good ductility, weldability and heat and electrical conductivity. It is commonly used in aluminum sheet fabrication and applications with modest load requirements.
1060 gains strength through cold working. Conventional solution treatment and aging do not provide the strengthening effect associated with alloys such as 6061-T6. Annealing restores ductility while reducing the strength gained through work hardening. Specify the grade, temper, thickness and fabrication requirements together. Compare 3003-H14 aluminum sheet for another non-heat-treatable option, or 6061-T6 aluminum plate when reviewing a heat-treatable engineering alloy.
Excellent Formability
Suitable for bending, stamping, deep drawing and spinning. O temper suits parts requiring substantial deformation; half-hard tempers suit general panels and routine sheet-metal forming.
Heat and Electrical Transfer
Suitable for heat-transfer plates, fins and appropriately designed conductive components. Electrical joints require consideration of oxide films, contact resistance and connection pressure.
Lightweight and Corrosion Resistant
A naturally formed oxide film provides good resistance in ordinary atmospheric conditions. Chloride exposure, strong acids or alkalis, and contact with dissimilar metals require separate assessment.
Decorative Finishing
Suitable for brushing, polishing, painting or anodizing. Appearance depends on the base surface, processing route and consistency between batches.
Welding and Assembly
Can be welded, riveted or mechanically joined using suitable processes. Control heat input when welding thin sheet to prevent burn-through and distortion.
Defined Strength Limits
Strength is lower than that of many alloyed aluminum grades. Increased hardness alone does not make it suitable for heavily loaded frames, wear parts or high-strength precision fixtures.
02 / TECHNICAL DATAChemical Composition & Physical Properties
Chemical Composition Reference
| Element | Mass fraction % | Element | Mass fraction % |
|---|---|---|---|
| Aluminum Al | ≥99.60 | Silicon Si | ≤0.25 |
| Iron Fe | ≤0.35 | Copper Cu | ≤0.05 |
| Manganese Mn | ≤0.03 | Magnesium Mg | ≤0.03 |
| Zinc Zn | ≤0.05 | Titanium Ti | ≤0.03 |
| Vanadium V | ≤0.05 | Other elements, each | ≤0.03 |
Individual impurity limits must not be added together as the actual composition; the minimum aluminum content must also be met. Batch acceptance is subject to the agreed standard and material test report.
Typical Physical Properties
| Property | Reference value | Selection guidance |
|---|---|---|
| Density at 20°C | 2,705 kg/m³; 2.70 g/cm³ commonly used for weight estimates | Useful for estimating plate weight and transport loads |
| Elastic modulus | Approximately 69 GPa | A harder temper does not produce a proportional increase in elastic stiffness |
| Thermal conductivity, O temper | Approximately 234 W/(m·K) | Supports preliminary selection for heat-transfer and cooling components |
| Electrical conductivity, O temper | Approximately 62% IACS | Relative to the International Annealed Copper Standard |
| Electrical resistivity, O temper | Approximately 0.0278 μΩ·m | Conductor design must also account for temperature and joint conditions |
| Thermal expansion, 20–100°C | Approximately 23.6 × 10⁻⁶/K | Allow for thermal movement during assembly |
| Magnetic behavior | Generally treated as non-magnetic in engineering applications | Suitable where a ferromagnetic base material is undesirable |
These are reference material properties, not guaranteed values for every batch. Temperature, temper and test conditions affect measured results.
03 / TEMPER SELECTIONMatch the Temper to the Process
| Temper | Meaning & characteristics | Typical selection direction |
|---|---|---|
| O | Annealed; high ductility and relatively low strength | Deep drawing, spinning and complex bending |
| H12 / H22 | Quarter-hard; strain hardened / strain hardened and partially annealed | Parts requiring a balance of formability and strength |
| H14 / H24 | Half-hard; produced through different processing routes | Nameplates, panels, general bending and sheet-metal parts |
| H16 / H26 | Three-quarter-hard; reduced ductility | Sheet parts requiring limited forming and greater resistance to permanent deformation |
| H18 | Full-hard; limited remaining formability | Predominantly flat parts and simple forming |
| H112 | Some strain hardening from shaping; mechanical properties controlled to specified requirements | Some thicker plates; verify requirements for the thickness and standard |
Mechanical Property Example: 2.0 mm Sheet
| Temper | Tensile strength Rm / MPa | Yield strength Rp0.2 / MPa | Elongation after fracture / % |
|---|---|---|---|
| O | 60–100 | ≥15 | ≥25 |
| H14 | 95–135 | ≥70 | ≥6 |
| H24 | 95–135 | ≥70 | ≥6 |
| H18 | ≥125 | ≥85 | ≥4 |
The values shown are a comparison for 2.0 mm sheet and do not apply to every thickness or standard. Elongation depends on gauge length, test direction and thickness. H24 is not inherently harder than H14; compare requirements under the same standard.
04 / DIMENSIONS & WEIGHTCommon Dimensions & Theoretical Weight
The following dimensions are common inquiry and selection examples, not a stock list. Confirm thickness, width, length and temper as a combination. Availability of large formats and thick plate requires separate confirmation.
| Category | Example inquiry dimensions, mm | Notes |
|---|---|---|
| Sheet thickness | 0.3 / 0.5 / 0.8 / 1.0 / 1.2 / 1.5 / 2.0 / 2.5 / 3.0 | Commonly used for stampings, panels and covers |
| Thicker plate | 4 / 5 / 6 / 8 / 10 / 12 / 15 / 20 | Example thicknesses; confirm temper and tolerances separately |
| Common full-sheet sizes | 1000 × 2000 / 1220 × 2440 / 1250 × 2500 | Width × length; confirm availability |
| Other inquiry sizes | 1500 × 3000, or cut to drawing | Confirm plate format, cutting allowance and dimensional accuracy |
| Surface & protection | Mill finish, protective film; other finishes by agreement | Specify one or both sides and requirements for each face |
| Thickness mm | Weight per area kg/m² | 1000 × 2000 mm / kg | 1220 × 2440 mm / kg |
|---|---|---|---|
| 0.5 | 1.35 | 2.70 | 4.02 |
| 1.0 | 2.70 | 5.40 | 8.04 |
| 2.0 | 5.40 | 10.80 | 16.07 |
| 3.0 | 8.10 | 16.20 | 24.11 |
| 5.0 | 13.50 | 27.00 | 40.19 |
| 10.0 | 27.00 | 54.00 | 80.37 |
The thickness boundary between sheet and plate depends on the applicable standard. Thickness tolerance, flatness and diagonal deviation cannot be expressed as one universal value; specify them in the order according to the standard, dimensions and accuracy class.
05 / APPLICATIONSTypical Uses & Selection Priorities
Electrical Components
Suitable for certain conductive links and electrical stampings. Specify conductivity, cross-section, temperature rise and connection method. Transformer windings generally use strip or foil in the appropriate dimensions.
Cooling & Heat Exchange
Used for heat-transfer plates, cooling fins and thermal assemblies. Assess thickness, effective area, contact thermal resistance and support conditions when determining performance.
Signs & Decorative Panels
Used for nameplates, signage, decorative backing and panels. Prioritize flatness, scratch limits, surface texture and coating adhesion.
Lighting & Reflectors
Can be formed into lampshades, lighting parts and surface-treated reflectors. Ordinary mill finish is not a mirror finish; specify and test reflectivity separately.
Stampings & Utensil Parts
A base material for deep-drawn or spun parts, trays and utensils. For food-contact applications, verify suitability of the finished article, coating and intended conditions of use.
Chemical Equipment Parts
May be considered for low-strength containers and liners where the material is compatible with the medium. Assess the chemical, concentration, temperature and pressure individually.
These are application selection guidelines. The grade does not automatically carry food-contact, pressure-equipment, marine or other specialized certification.
06 / FABRICATION & FINISHFabrication & Surface Options
Match the Temper to Your Process
- Bending: Select the inside bend radius according to temper, thickness, rolling direction and tooling. Trial forming is advisable for complex parts.
- Deep drawing & spinning: Evaluate O temper first, and control lubrication, blank-holder force, deformation and intermediate annealing.
- Machining: Soft tempers can cause tool buildup and burrs. Use sharp tools, suitable lubrication and appropriate workholding.
- Welding: Remove oil and oxide films, and select compatible filler and shielding gas. The heat-affected zone of strain-hardened material may soften.
- Precision fabrication: Control clamping distortion in thin sheet. Define inspection conditions after machining when flatness is critical.
| Surface option | Features & uses | Items to specify |
|---|---|---|
| Mill finish | Retains rolling texture; suitable for general industrial fabrication | Permitted oil film, scratches and color variation |
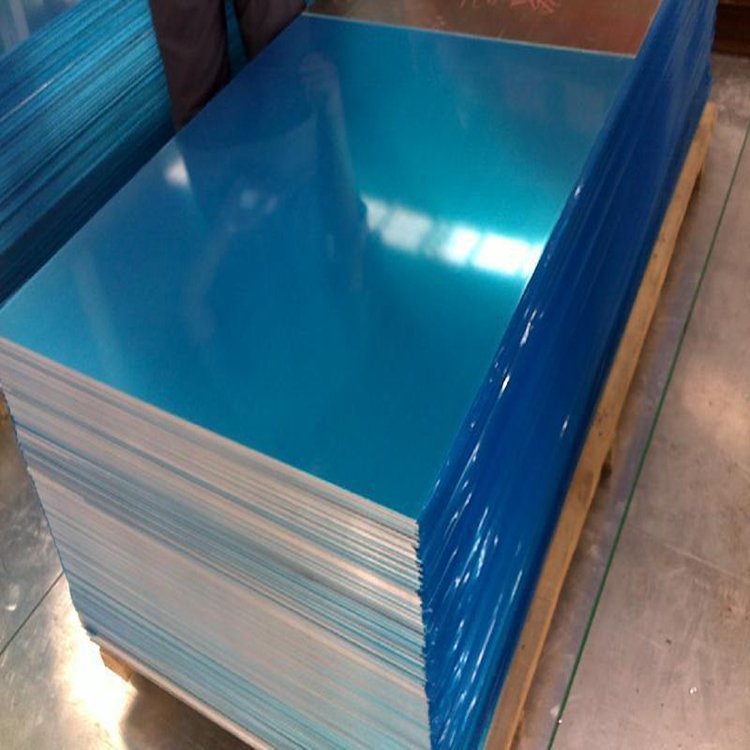
| Protective film | Reduces surface scuffing during handling and fabrication | One or both sides, film type, process compatibility and removal deadline |
| Brushed / polished | Provides a directional texture or higher gloss | Texture direction, roughness, gloss and reference sample |
| Anodized | Improves surface protection and decorative appearance | Film thickness, color, sealing and batch-to-batch variation |
| Painted / color coated | For panels requiring color and surface protection | Coating system, color, film thickness and adhesion |
07 / PACKING & INSPECTIONPacking, Storage & Quality Checks
Packing Recommendations
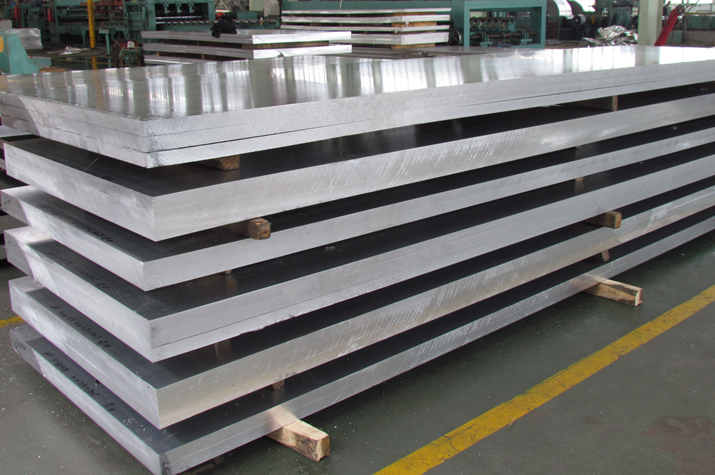
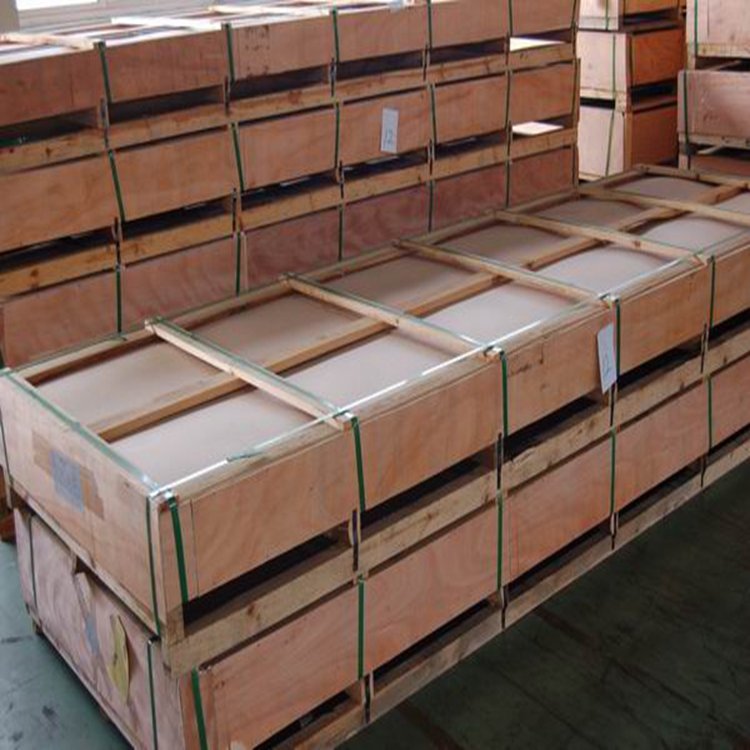
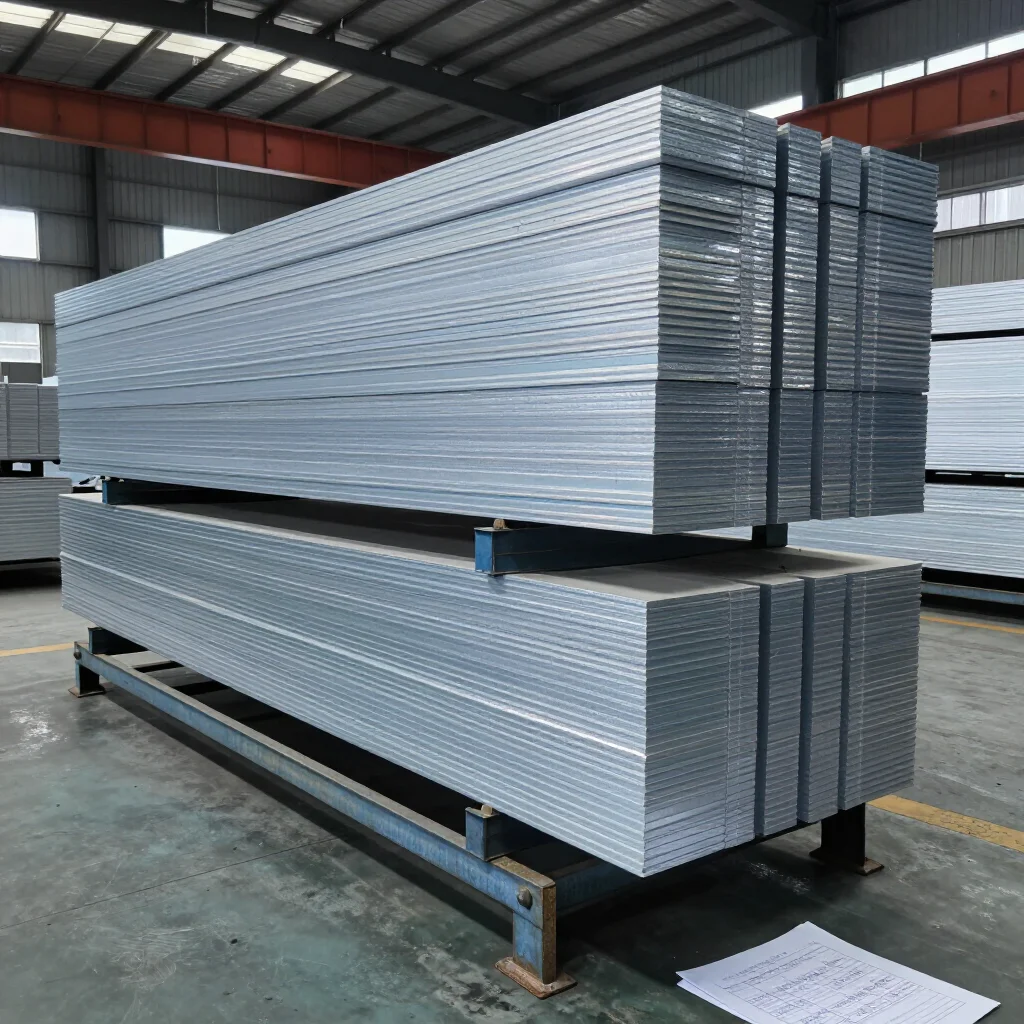
Select pallets or wooden crates according to plate dimensions and transport method, with interleaving paper, edge protection, moisture-resistant wrapping and strapping as appropriate. Prevent movement while avoiding edge damage from excessive strapping pressure.
Storage & Handling
Store level and stable in a dry indoor area. Prevent rain, condensation and debris from entering between sheets. After a large temperature change, allow the packaged material to approach ambient temperature before opening to reduce condensation. Avoid dragging across plate surfaces.
Incoming Inspection
Check grade, temper, heat or batch number, quantity, thickness and sheet dimensions. Inspect scratches, dents, edge burrs, water staining and packaging damage. Agree on an approved reference sample in advance when appearance is critical.
08 / FREQUENTLY ASKED QUESTIONSMaterial Selection FAQs
How do 1060 and 1050 differ?
One key difference is minimum aluminum content: 99.60% for 1060 and 99.50% for 1050. Both are commercially pure aluminum, but purity alone does not determine every property. Compare temper, standard and actual test data as well.
Can 1060 replace 3003, 5052 or 6061?
Do not substitute based on dimensions alone. Designs requiring higher strength, fatigue performance, resistance to a specific corrosive environment or precision structural performance need a fresh review of alloy properties and joining requirements. 1060 is better suited to applications prioritizing ductility and thermal or electrical conductivity.
Is a harder temper always stiffer?
A harder temper generally has higher yield strength and better resistance to permanent deformation, but the elastic modulus of the same alloy changes very little. Elastic deflection also depends primarily on thickness, span and support conditions.
Can heat treatment increase its hardness?
1060 is not strengthened by solution treatment and aging. Strengthening mainly comes from cold working; annealing generally reduces hardness and improves ductility.
Is it ready for mirror-finish or precision electrical applications?
Additional specifications are required. Mirror-finish applications need agreed gloss, reflectivity and surface-defect limits. Electrical applications need specified conductivity, dimensions, burr limits and connection-surface quality, rather than the grade alone.
09 / ORDERING GUIDEComplete Specifications for Accurate Selection
Please include: Grade + temper + thickness × width × length + quantity + surface requirements + application + governing standard and tolerances.
Example order description: 1060-H24 aluminum sheet, 2.0 × 1220 × 2440 mm, 100 sheets, protective film on one side, for bent panels. Thickness tolerance, flatness, material test report and packing method to be agreed.
The contract may specify applicable parts and editions of ASTM B209/B209M or GB/T 3880, with chemical composition, mechanical properties, testing and dimensional requirements clearly defined. Stock, prices, minimum order quantity, available dimensions and lead time are subject to the actual quotation.
Reviews
There are no reviews yet.